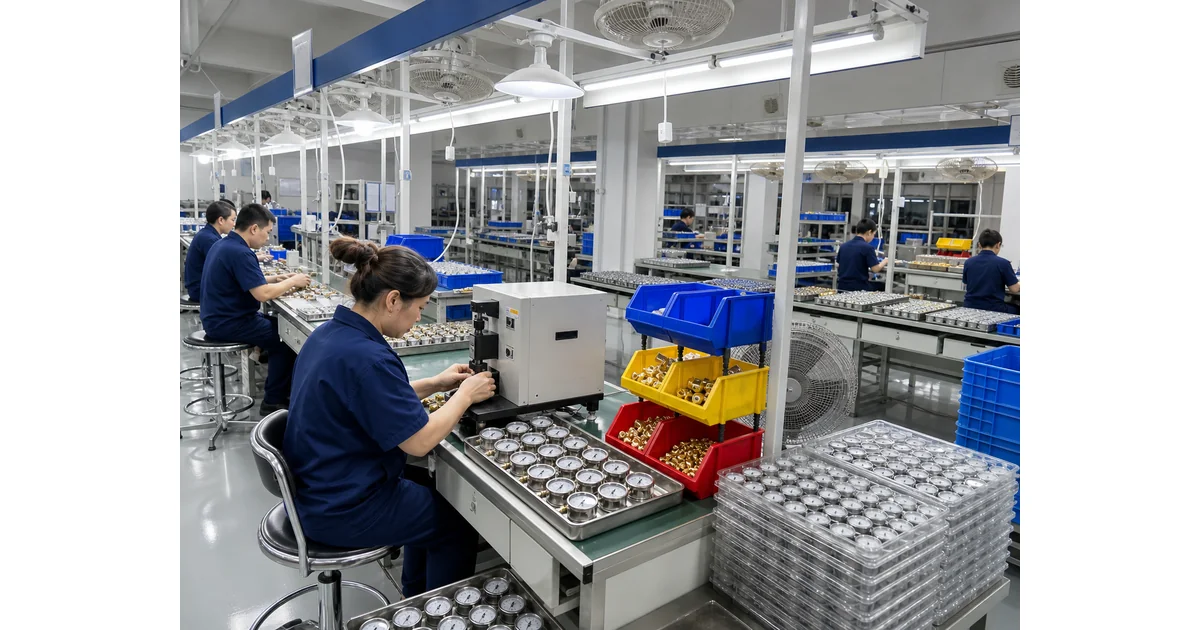
Industrial heat pump pressure monitoring connects mechanical gauges, pressure transmitters and differential pressure checks to the water, refrigerant and service loops that move heat through a plant. As factories, district heating networks and commercial buildings electrify heat, the pressure instrumentation must support commissioning, efficiency checks and maintenance without pretending to replace the heat pump OEM controls.
Why industrial heat pump pressure monitoring matters in retrofit projects

Industrial heat pump pressure monitoring means choosing pressure gauges, transmitters and differential pressure instruments so operators can verify flow conditions, pump head, filter loading, heat-exchanger pressure drop and safe isolation points. Heat pumps are becoming a central heating technology: the International Energy Agency describes them as important for secure and sustainable heating, while the European Commission notes that heat pumps can be around three to five times more energy efficient than gas boilers under suitable conditions. Those energy claims depend on the whole system, not on one pressure instrument.
In a retrofit, pressure monitoring is often added to old pipework, existing pumps and new packaged equipment. The instrument plan should answer practical questions: is the evaporator loop flowing, is a strainer blocking, is the condenser loop balanced, can maintenance isolate and verify zero pressure, and can the building management system trend abnormal pressure changes?
For adjacent fundamentals, see the pressure transmitter vs pressure gauge selection guide and the industrial pressure gauge selection guide.
Review Industrial Pressure Gauge Options ->Explore 143+ industrial gauge models→Where to measure pressure in an industrial heat pump system
A heat pump skid normally includes internal sensors selected by the OEM. Plant instrumentation adds accessible local indication and external trend points around the skid. Useful measurement points include pump suction and discharge, inlet and outlet of plate heat exchangers, strainers or filters, expansion vessels, make-up water, buffer tanks and isolation manifolds.
Do not place instruments only where the pipe is convenient. A gauge downstream of a throttling valve may tell a different story from one at pump discharge. A differential pressure reading across a heat exchanger or filter is often more useful than two isolated absolute readings because it directly shows fouling, blockage or flow restriction.
| Monitoring point | Typical purpose | Instrument option |
|---|---|---|
| Pump suction and discharge | Confirm pump head and cavitation risk | Gauge pair or transmitters |
| Plate heat exchanger | Watch fouling and flow restriction | Differential pressure gauge or two transmitters |
| Strainer or filter | Trigger cleaning before flow drops | Differential pressure switch, gauge or transmitter |
| Expansion vessel and make-up line | Verify static fill pressure | Local gauge plus service valve |
| Refrigerant service points | OEM/service diagnostics only | Rated service instruments under approved procedure |
Gauge, transmitter and differential pressure choices
A mechanical pressure gauge gives a fast local reference during maintenance, flushing and manual valve operation. A pressure transmitter sends a continuous signal to a PLC, BMS or data logger. Differential pressure instruments compare two points and are often the best choice for filters, strainers and heat exchangers.
The right choice depends on the decision being made. If a technician only needs to verify zero pressure before opening a strainer, a local gauge with a proper isolation valve may be enough. If the owner wants alarms, trend history or energy diagnostics, a transmitter is usually needed. For fouling, a differential reading is clearer than asking operators to subtract two gauge values.
Manogauge can supply mechanical gauge families and instrumentation assemblies from Zhejiang manufacturing resources, but final selection must follow the heat pump OEM manual, site piping class and project documentation. Do not add a transmitter into a refrigerant circuit unless the connection, refrigerant compatibility, pressure rating and service procedure are approved.
Request a Heat Pump Instrument ChecklistOur engineers respond within 24 hours→Selecting range, wetted material, connection and protection
Start with pressure range. For steady service, choose a range that keeps normal operating pressure in a readable part of the scale while still covering startup, pump shut-off head and expected abnormal conditions. A common engineering target is to avoid operating continuously at the extreme top of the scale, but the final range must be checked against site design pressure and applicable gauge standard practice such as EN 837 or ASME B40.100.
Wetted material is a compatibility decision. Hydronic loops may contain glycol, corrosion inhibitors, cleaning chemicals or low-conductivity water. Brass may be acceptable in some building-water loops, while stainless steel is often preferred where corrosion resistance, condensate chemistry or longer service life matter. Seals, gaskets and fill fluids also need compatibility checks.
Specify the connection carefully: NPT, BSP, G or metric threads are not interchangeable. Add isolation valves for calibration and replacement, use siphons only where hot media require thermal protection, and consider snubbers only when pump pulsation or vibration makes readings unstable. For dirty water, a diaphragm seal or flush connection may be more reliable than a small blocked pressure port.
Installation and commissioning checks for reliable readings
Installation quality often decides whether the pressure data is useful. Mount gauges upright and readable from a safe walkway. Avoid unsupported branch connections that let the gauge act as a lever. Keep transmitters away from avoidable heat, water ingress and cable strain. On low points where air or sediment can collect, verify whether the impulse line arrangement will trap gas, dirt or stagnant liquid.
- Confirm the P&ID tag, pressure range, design pressure and temperature.
- Match wetted material, seal material and thread to the actual loop fluid.
- Install isolation valves and, where needed, vent or drain arrangements.
- Commission with gradual pressurisation and leak checks from a safe position.
- Compare local gauges with transmitter values and record zero/span checks.
- Define alarm thresholds only after normal operating data is available.
For installation basics that apply beyond heat pumps, review pressure gauge installation best practices and pressure gauge snubber selection for pulsation protection.
Limits, faults and procurement questions before ordering
Pressure monitoring cannot prove that a heat pump is efficient, correctly charged, safe for refrigerant service or compliant with local code. It also cannot diagnose every compressor, expansion valve or controls fault. It supplies evidence: pressure trend, pump head, static fill pressure, pressure drop and abnormal changes that engineers can interpret with temperature, flow, electrical and OEM fault data.
Warning signs include rising differential pressure across a strainer, falling pump discharge pressure, large disagreement between a gauge and transmitter, pointer vibration, leakage at a threaded joint, or a transmitter drifting after repeated freeze or overpressure events. Any instrument exposed to high pressure, refrigerant, hot water, glycol, corrosive additives or hazardous locations needs engineering review before reuse.
Before ordering, provide the loop fluid, maximum and normal pressure, temperature, connection thread, required signal, ingress protection, accuracy requirement, mounting position, isolation method and documentation needs. A careful industrial heat pump pressure monitoring specification prevents mismatched gauges and makes commissioning data easier to trust.
Commissioning data makes heat-pump pressure monitoring useful. Record suction and discharge pressure with leaving-water temperature, entering-water temperature, ambient condition, compressor speed and operating mode. A pressure value without refrigerant temperature cannot establish superheat or subcooling, and a gauge alone cannot diagnose charge, restriction or compressor health. Use the equipment manufacturer's envelope and the actual refrigerant designation when defining alarm limits.
Retrofit systems need particular care at transition points: old service valves, brazed adapters, vibration, oil return and limited clearance can all affect the measurement. Confirm whether the instrument sees refrigerant, water or glycol; the wetted materials and connection are different decisions. Where a transmitter feeds control logic, define signal scaling, loss-of-signal behaviour and calibration access separately from the local dial gauge.
For industrial heat pump pressure monitoring, the RFQ should include refrigerant, low and high operating pressures, maximum credible pressure, temperature, port location, vibration, range, accuracy and required documentation. Confirm the final alarm and safety limits with the heat-pump designer; monitoring hardware does not replace the unit's protective controls.
Define the measurement point in the commissioning record: compressor suction, discharge, liquid line or water circuit. A common connection thread does not make those points interchangeable because the pressure, temperature and medium differ. Check pulsation, vibration and service access, then verify the zero reading and response after the system reaches steady state. Trend pressure together with temperature and compressor speed so a future deviation has context.
Any alarm limit must come from the heat-pump design and refrigerant envelope. A local gauge is useful for inspection, but it is not a substitute for the unit's pressure switch, relief device or control logic.
How to turn refrigerant circuit pressure, operating envelope, temperature compensation, service ports and alarm limits into a purchase specification
A useful specification begins with the process rather than the catalogue name. Record the normal operating value, the minimum and maximum credible values, the upset condition, the medium composition, the process temperature and the way the instrument will be mounted. Then state what the operator must see: a stable local indication, a peak, a differential, a switch point or a value that will be compared with a calibrated reference. This distinction matters because a gauge can be mechanically accurate yet unsuitable when its sensing element, connection or response is wrong for the installation.
Separate the continuously expected condition from the short duration event. For refrigerant circuit pressure, operating envelope, temperature compensation, service ports and alarm limits, the short event may be more important than the average reading, but it should not be handled by quietly selecting a larger dial range. A larger range reduces readability and can increase the error at the operating point. Conversely, a range selected too tightly can expose the element to repeated overload. Document the expected cycle, the allowable overpressure and the required indication during start-up, shutdown and cleaning. If those values are unavailable, the final range must remain a site-engineering decision.
Installation details deserve the same attention as the gauge body. Confirm whether the tapping point is exposed to vibration, pulsation, water hammer, thermal shock, condensation, washdown or a corrosive atmosphere. Provide an isolation valve where safe maintenance requires it, and consider a gauge cock, siphon, snubber, diaphragm seal or remote mounting only when its effect on response and calibration is understood. The connection thread must match the mating component; NPT, BSP/G and metric threads are not interchangeable simply because their nominal size appears similar. Never force a mismatched thread or use sealant to compensate for the wrong standard.
Before release, ask for the evidence that is actually needed for the job: dimensional drawing, wetted-material declaration, accuracy statement, calibration method, pressure test requirement and packing or cleanliness instruction. Do not request certificates as a substitute for checking the process chemistry or hazard classification. Standards and customer specifications may define construction, testing or documentation, but they do not automatically prove compatibility with every concentration, temperature or cleaning cycle. The responsible engineer should reconcile the instrument data sheet with the P&ID, valve arrangement and maintenance procedure.
Commissioning should establish a baseline. With the process in a known condition, record the gauge indication, reference reading, temperature, pump or compressor state and any pointer oscillation. Recheck after the system reaches normal load and after a controlled shutdown. A drifting zero, a slow response, a blocked impulse path or an unexpectedly quiet pointer can all be failure signals rather than evidence of good performance. Trend records also make later replacement decisions more reliable because the next instrument can be specified from observed service instead of a generic catalogue assumption.
The practical conclusion for refrigerant circuit pressure, operating envelope, temperature compensation, service ports and alarm limits is to select the complete measurement chain: sensing element, wetted material, range, accuracy, connection, mounting, protection accessory and documentation. The product photograph on this page identifies the real Manogauge gauge construction used as a reference; it is not proof that the same configuration is correct for every medium or pressure. Confirm the final model, dimensions and available options against the current data sheet before purchase.
Review note: Treat the published values as a framework for engineering review, not as a universal approval. The final choice should be checked against the current Manogauge data sheet, the project P&ID and the site risk assessment. Record any deviations, accessory settings and inspection interval in the maintenance file so that a replacement gauge is not selected from a photograph alone.
Key takeaways
- Pressure monitoring in heat pump retrofits should verify flow, pressure drop, pump head and safe maintenance points, not replace OEM controls.
- Use gauges for local service checks, transmitters for trend data, and differential pressure instruments for filters and heat exchangers.
- Range, wetted material, thread, isolation, ingress protection and commissioning records must be confirmed before ordering.
Frequently asked questions
What pressure points are most useful on an industrial heat pump?
Pump suction and discharge, heat-exchanger inlet/outlet, strainer or filter differential pressure, expansion vessel pressure and make-up water pressure are usually high-value points. Refrigerant pressure points should follow the OEM service procedure only.
Should a heat pump use gauges or pressure transmitters?
Use both when the operating decision needs both local visibility and trend data. A gauge helps maintenance verify pressure at the equipment; a transmitter lets the BMS or PLC trend pressure, alarm abnormal changes and compare pressure with temperature or flow.
How do I choose the pressure gauge range?
Confirm normal pressure, startup pressure, pump shut-off head, design pressure and safety margin. The gauge should be readable during normal operation and still rated for expected maximum conditions; final range must match the project specification.
Is stainless steel always required?
No. Material depends on water chemistry, glycol, corrosion inhibitors, cleaning chemicals, temperature and outdoor exposure. Stainless steel is often preferred for corrosion resistance, but compatibility must still be verified.
Can pressure monitoring prove heat pump efficiency?
No. Pressure data helps diagnose flow restriction, pump head and fouling, but efficiency also requires temperature, flow, electrical power, refrigerant-side data and OEM performance logic.